Fasteners can look interchangeable in a shipment crate, but a small mismatch in grade, coating, or thread can stop a delivery at inspection. How to ensure fasteners meet international export standards begins with identifying the destination market, end use, and buyer’s specification. Requirements may differ for structural bolts, stainless-steel screws, and coated components. The relevant references can include ISO 898-1 for mechanical properties of carbon-steel fasteners, ISO 3506 for corrosion-resistant stainless-steel fasteners, and ISO 4042 for electroplated coatings. One standard rarely answers every question.
The ISO Survey 2022 reported more than 1.2 million ISO 9001 certificates worldwide, showing how widely quality-management systems are used. But an ISO 9001 certificate does not prove that a particular fastener meets its required dimensions, strength, or coating specification. That distinction matters. This guide explains how exporters can verify applicable standards, assess supplier documentation, and plan sampling and inspection. It also considers material certificates, traceability, marking, packaging, and test reports, including checks for consistency between documents and the actual goods. Standards such as ISO 3269 provide guidance for acceptance inspection, while customer contracts may set additional requirements. A report can be complete and still leave uncertainty if its batch number does not match the carton label. I have seen that detail underestimated. Export compliance is not a paperwork exercise alone; it depends on clear specifications, reliable testing, and records that follow each lot from production to shipment.
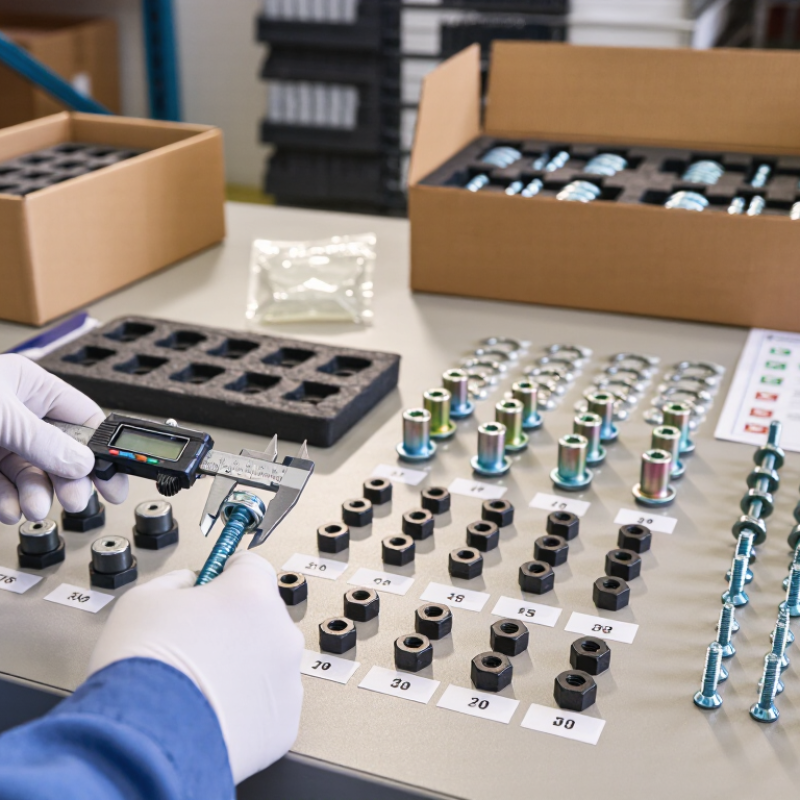
Before shipping fasteners, identify the exact requirements of the destination country and intended application. A bolt used in construction may face different rules from one used in machinery. Ask the importer which national standards, certification marks, and inspection documents customs or buyers expect. Do not assume that an ISO reference alone guarantees acceptance. Countries may adopt different editions or require local testing.
Check material grade, dimensions, mechanical properties, coatings, labeling, and language requirements against the destination’s current rules. For example, ISO 898-1 specifies mechanical properties for carbon and alloy steel fasteners; property class 8.8 has a nominal tensile strength of 800 MPa. That figure is a useful technical reference, not automatic proof of compliance in every market. Small details matter. A coating or package label can trigger extra questions.
Use the importing country’s standards body, customs guidance, and an accredited testing laboratory to verify requirements before production. The WTO’s 2023 Technical Barriers to Trade Annual Review recorded more than 4,000 new notifications across product sectors; these were not fastener-specific, but show why checks need to be current. Keep test reports, material certificates, and product drawings linked to each shipment. A spreadsheet can still miss a local amendment. Recheck the details with the importer before the order is packed.
| Importing market | Typical standards or regulations to check | Common compliance evidence | Key checks before shipment |
|---|---|---|---|
| United States | The specification depends on the fastener and its use. Common examples include ASTM A307 for certain carbon-steel bolts and studs, ASTM F3125 for specified structural bolts, and ASTM F593/F594 for stainless-steel bolts and nuts. | Mill test reports or material certificates, dimensional and mechanical test results, and coating records when specified by the purchase order or applicable standard. | Confirm the exact ASTM grade, diameter, thread, mechanical properties, coating, and any project or state requirements. Do not assume one ASTM specification covers every fastener application. |
| European Union | For construction use, check the applicable harmonised product specification and the Construction Products Regulation. Examples for structural bolting include EN 15048 for non-preloaded assemblies and EN 14399 for preloaded assemblies. | Where the product is covered by an applicable harmonised specification, the required Declaration of Performance and CE marking; supporting product and test documentation as applicable. | CE marking is not a blanket requirement for every ordinary fastener. Verify the product’s intended construction use and the current applicable harmonised specification before making a marking claim. |
| United Kingdom | Check the relevant British Standard or BS EN product specification for the intended application. Structural bolting specifications commonly include BS EN 15048 and BS EN 14399. | Product conformity documents, test records, and construction-product declarations or markings where required by the applicable rules in the destination territory. | Confirm whether the destination is Great Britain or Northern Ireland and check the current construction-products marking and documentation rules for that territory. |
| Canada | For structural applications, check the governing building code and design standard, such as CSA S16, together with the bolt and material specifications referenced by the project documents. | Material certificates, mechanical test results, dimensional inspection records, and traceability documents as required by the project specification or purchaser. | Requirements can vary by province, building code, and application. Confirm the specified bolt standard, grade, assembly requirements, and acceptance criteria with the project documents. |
| Australia and New Zealand | For structural steelwork, check the applicable building requirements and standards, including AS/NZS 1252.1 for high-strength structural bolting assemblies where specified. | Assembly identification, material and test certificates, and inspection records required by the applicable standard and project specification. | Verify whether the order requires a complete bolting assembly, the specified property class and coating, and compliance with the current edition of the applicable standard. |
| Japan | Check the Japanese Industrial Standards (JIS) specified by the purchaser or applicable project documents. The required JIS depends on fastener type, material, dimensions, and intended use. | Inspection certificates, material and mechanical test results, dimensional records, and traceability information as stated in the order. | Confirm the exact JIS designation and edition, metric dimensions and tolerances, strength class, surface treatment, and Japanese-language documentation needs. |
Requirements depend on fastener type, intended use, contract specifications, and current local regulations. Confirm the applicable standard and edition with the importer or project authority, and separately verify customs classification, country-of-origin marking, and shipping-document requirements.
State the thread size and pitch, length, property class, material, coating, and dimensional tolerances. Small details matter.
Buyers and destinations may require different editions or extra details. Installation conditions and customer drawings can also change requirements.
Not by itself. Match the certificate’s heat number and grade to the order, markings, and production lot. It is easy to assume too much.
Use calibrated gauges for thread diameter and pitch. Check length, head dimensions, and coating buildup with suitable measuring tools.
It has a minimum tensile strength of 800 MPa. The test method and sampling plan still need to be specified.
They help connect inspection results to the fasteners actually produced. Keep the lot number, sample, and test records together.
No. A single result may miss variation across a batch. Check the sampling plan and review actual laboratory results.
Review calibration records, test-piece identification, material evidence, and any heat-treatment or coating changes. I would not rely on a certificate alone.
How to ensure fasteners meet international export standards begins with understanding the requirements of the destination country, since specifications for materials, dimensions, testing, and documentation can differ by market. Exporters should identify the applicable standards and product specifications before production, then confirm that each fastener’s material composition, measurements, and mechanical performance meet those requirements. Clear specifications help prevent mismatches between the product, customer expectations, and import requirements.
Compliance also depends on consistent testing and reliable records. Maintain traceable documentation linking test results and material information to the relevant production batches, and review records before shipment. Finally, check that product markings are accurate and that packaging protects fasteners during handling and transport. Prepare complete export documents, ensuring they describe the goods consistently and include any required certificates or inspection records. A careful process from specification review through shipment helps reduce delays and supports dependable access to international markets.

 VLC Part